

INDUSTRIAL ROBOTICS AND THE PHARMACEUTICAL INDUSTRY
The pharmaceutical industry is the manufacturing field with the highest growth in the decade of 2008-2018 in Italy. Exports increased by 100% while production increased by 22%, as opposed to the rest of the Italian manufacturing industry which suffered a -14% decline over the same period. The data, therefore, speak clearly.
This positive trend is determined both by market demands and by the industry's ability to always look with great interest and foresight at technological innovation and in particular at the application of industrial robotics in many key processes. In addition, the pharmaceutical segment is investing heavily in innovation and research and development projects to become more efficient, safer and sustainable every day.
Industrial robots for the pharmaceutical field
Let's start from an inhered characteristic of robotic cells: the possibility of guaranteeing very high, constant and repeatable quality standards over time. Let's now link it to a key aspect of the chemical-pharmaceutical field, namely the need to meet very demanding quality standards, especially in terms of accuracy, hygiene and precision.
The benefits that robotic cells, and more generally industrial robotics at 360°, can bring to such a complex field are immediately evident.
Robotic cells become an essential help in tasks like:
- Respect for hygiene measures
- Constant supervision
- Quality control
The normatives that chemical-pharmaceutical products must comply with in order to be market-compliant are very stringent, and technological innovation is a key element in complying with them as much as possible. Let's see how industrial robots are applied in pharmaceutical production processes.
Industrial robots can manage:
- Medicines production (e.g. robots can mix)
- Products packaging (e.g. robots can count extremely small objects, dispense liquids or powders, package and box)
- Quality control through inspection with integrated vision systems
Robots, through automated tasks, then deliver consistent and repeatable results, speed up the production flow and absolve staff of potentially risky and time-consuming tasks.
How are robots for the pharmaceutical field made?
Robots and robotic cells that are installed inside pharmaceutical industries must have some peculiar features, which are not always required in every productive field. Here are a few:
- It is important that surfaces are resistant to aggressive and decontaminant treatments
- They must be compact and have a limited reach
- Surfaces must be smooth to prevent bacteria from lurking in rough surfaces, edges or protrusions
The most utilized robots in this field are cobots, namely collaborative robots created to work in contact with men. Cobots, generally, can only move around people at certain levels of speed and must avoid human contact (if contact does happen, they react by stopping or changing their direction). In compliance with these requirements, the use in the chemical-medical-pharmaceutical field is considerable, even in case of small-medium companies, because they are safe, flexible and have manageable costs.
By their side there are certainly anthropomorphic robots, obviously with the characteristics specified right above.
What are the benefits of robotics in the pharmaceutical industry?
We have already met a few, but since they have a crucial role in the quality of production in such a demanding field, here are all the benefits of industrial robotics in the pharmaceutical field:
- Optimized managing of production
- Guaranteed aseptic processing
- possibility of complete sanitization of the automated system
- Quality control and high precision conformity
- Data gathering in real time
- Better working conditions and increased safety for employees
- Speeding of the productive flow
Robotic cells for the pharmaceutical industry
The robotic cells used in chemical-pharmaceutical companies in the production of drugs and their derivatives are mainly cells for handling, dosing and quality control.
The new frontiers of scientific research expand the possible applications of automated cells in the pharmaceutical world, such as the manipulation of cell cultures.Industrial robots used in these particular activities must meet strict construction requirements that ensure maximum precision, repeatability and hygiene. These are industrial robots subjected to special coating treatments, VHP (Vaporized Hydrogen Peroxide) resistant, Clean Robot Technology (ISO Class 1).
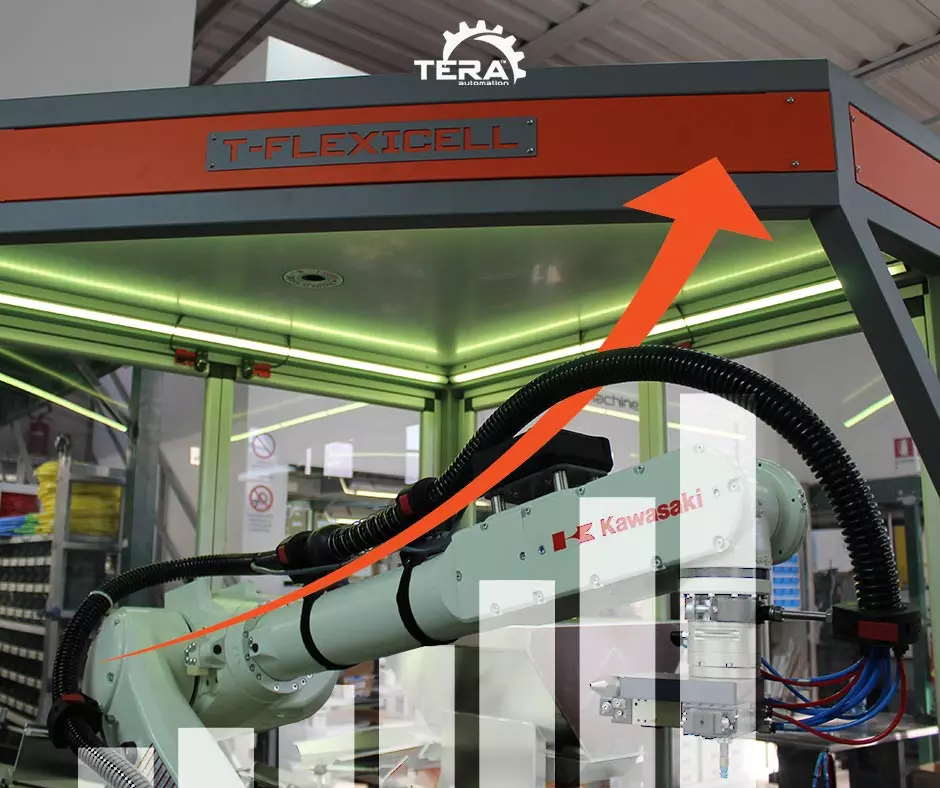
As a System Integrator, the design of a robotic cell like, for example, our T-Flexicell Pharma, requires extreme attention to the particularity of the environments in which it will be installed. For example, it is often necessary to use electric actuators as opposed to pneumatic solutions, as well as the execution of treatments with acid-proof epoxy resins for the entire cell.
Ultimately, it can be affirmed that the pharmaceutical sector, although with its peculiarities in terms of general requirements and specificity of the work environment, is very suitable for the use of automated solutions, robots, vision systems and the many variants of custom solutions.